Cutting speed (Vc) is the relative surface speed between a cutting edge and the workpiece, usually expressed in metres per minute (m/min) or surface feet per minute (ft/min, SFM). It is not spindle speed in rpm or feed rate. To choose Vc, start with the cutting-tool manufacturer’s data for the specific workpiece material, tool, and operation, then account for diameter, engagement, and setup stability.
What is cutting speed (Vc)?
Vc describes how quickly the cutting edge moves across the surface being cut. In turning, it refers to the workpiece surface passing the tool; in milling and drilling, it describes the cutting speed at the tool’s cutting diameter. The usual units are m/min or ft/min (SFM).
As an Amazon Associate I earn from qualifying purchases.
Vc is distinct from spindle speed. Spindle speed, written as n, is the number of spindle revolutions per minute (rpm). The same Vc requires a different rpm at different diameters: a smaller diameter must rotate faster to produce the same surface speed. Sandvik Coromant documents the turning relationship between surface speed, machined diameter, and spindle rpm in its turning formulas and definitions.
How do I calculate spindle speed from cutting speed?
Use the cutting speed and the diameter at the cutting interface. For turning, use the machined diameter; for milling or drilling, use the tool’s cutting diameter for the applicable calculation.
#1 Best Overall

- [DEBURRING TOOL KIT] Includes 1 BS1010 blades made of M2 High-Speed Steel (HSS). Each blade is tempered to HRC 62–64 for industrial-grade wear resistance. The M2 blades maintain a sharp cutting edge up to 80% longer than standard carbon steel when processing stainless steel, aluminum, and hard metals.
- Metric: n (rpm) = [Vc (m/min) × 1000] / [π × D (mm)]
- Inch units: n (rpm) = [Vc (ft/min) × 12] / [π × D (in)]
Here, D is the relevant diameter and π is approximately 3.1416. The factor 1000 converts metres to millimetres; 12 converts feet to inches.
Formula example (arithmetic only)
If Vc is 100 m/min and the cutting diameter is 10 mm, n = (100 × 1000) / (π × 10), or approximately 3,183 rpm. This calculation demonstrates the formula only; it does not mean 100 m/min is suitable for any particular tool, material, machine, or operation.
Rank #2
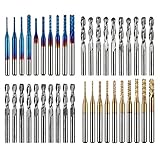
- High Quality: The Genmitsu end mills are made of ultra-fine 0.2μm tungsten carbide steel alloy that can keep continuous machining 800 minutes. Moreover, its Nano Blue Coating /Titanium Coating with high hardness and heat resistance enables the tool's cutting edge to retain crucial sharpness and lubricity. This provides longevity and produces cutting results of the highest quality.
- 2-Flute Spiral Flat Nose & Ball Nose End Mills -- Shank Diameter: 3.175mm, Cutting Diameter: 3.175mm, Cutting Length: 17mm, Overall Length: 38mm.
- Two End Mill Sets -- Shank Diameter: 3.175mm, Cutting Diameter: 0.8 - 3.0mm (0.8/1.0/1.2/1.4/1.6/1.8/2.0/2.2/2.5/3.0mm), Cutting Length: 17mm, Overall Length: 38mm, with Nano blue and Titanium coating.
- Applicable Materials: Widely used in various materials including plastics, aluminum, circuit board, wood, as well as other precision parts processing.
- Wide Compatibility: The MC40A end mills are compatible with most desktop CNC machines, such as the Genmitsu 3018 Series, as well as other industrial CNC machines. Just make sure you select the correct-sized collet for your device
Haas Automation’s Indexable Drills, Speeds and Feeds, Inch provides the inch-unit cutting-speed and spindle-speed relationships in its drill guide.
Quick wins for a faster PC:
Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Repair Windows errors before they cause bigger problemsFix Now →How do I choose the right cutting speed for a material?
There is no single Vc that is right for every material or CNC setup. Use the toolmaker’s cutting-data chart or calculator for the exact tool and operation, and treat its recommended speed as a starting point under the stated conditions.
Rank #3

- 360° Articulating Head – Swivels to reach edges, cross bores, and recessed areas that standard deburrers can't access. Perfect for complex 3D prints and machined parts
- 20-Piece M2 HSS Blade Kit – Includes 10x BS1010 for standard holes + 10x BK3010 specifically for small-diameter holes. Long-lasting sharpness for hundreds of uses
- CNC Blue Anodized Aluminum Handle – Lightweight, corrosion-resistant, with a comfortable non-slip grip. The striking blue finish adds style to your workshop
- Versatile Material Compatibility – Works flawlessly on 3D prints (PLA/ABS/Resin), aluminum, copper, PVC, soft metals, and plastics. A must-have for makers, machinists and 3D printing hobbyists
- Complete Kit with Storage Case – Includes durable case to keep all 20 blades organized and secure. Tool-free blade replacement with built-in chuck
- Identify the workpiece material and condition. Check the material description and, where relevant, hardness. Find the material group used by the toolmaker rather than relying on a broad label such as “steel.”
- Match the tool and operation. Look up the tool family, grade, geometry, and diameter, along with whether the work is turning, milling, or drilling. Data for one tool or operation should not be assumed to apply to another.
- Read the full recommendation. Separate Vc from feed per tooth or feed per revolution, and note whether the listed speed is a minimum, starting value, or maximum. Check any stated assumptions or adjustment factors.
- Account for engagement and stability. Radial and axial engagement, rigidity, and cut stability can affect appropriate cutting conditions. For milling, consult the toolmaker’s engagement guidance; do not apply a speed or feed adjustment from one product family as a universal rule.
- Start within the recommended range and assess the cut. Consider chip formation, tool wear, finish, sound, and machine load while staying within the tool and machine limits. Make adjustments using the maker’s data and the actual behavior of the setup.
Example: a product-specific milling value
Kennametal’s GOmill PRO metric data for regular-tool side milling in material group P5 lists a Vc range of 60–100 m/min, with 80 m/min as the starting value. The table also gives feed recommendations by diameter and says to reduce feed per tooth by 20% for slotting. Those figures apply to the named GOmill PRO family and its stated conditions—not to every steel, end mill, or milling setup. See the GOmill PRO technical data for the relevant chart and engagement factors.
Why recommendations may differ
Before comparing two cutting-speed figures, align the conditions they describe:
Rank #4

- [DEBURRING TOOL KIT] Includes 11 BS1010 blades made of M2 High-Speed Steel (HSS). Each blade is tempered to HRC 62–64 for industrial-grade wear resistance. These M2 blades maintain a sharp cutting edge up to 80% longer than standard carbon steel when processing stainless steel, aluminum, copper, brass, PVC, and other hard materials
- [RED ANODIZED CNC HANDLE] The 5.4 inch handle is precision-engineered from aluminum via CNC machining with a premium red anodized finish. Its knurled grip texture provides a stable, non-slip hold for improved handling during detailed edge work. The compact body has a slightly heavier feel for steadier control during deburring, pipe cleanup, and metal edge finishing
- [360° SWIVEL MECHANISM] Features a high-precision internal swivel mechanism that allows the blade to rotate effortlessly within the handle housing. This fluid internal movement helps the blade track curves, holes, edges, and inside diameters naturally for a cleaner finish. Includes a spring-loaded collar for secure retention and rapid blade changes
- [3D PRINTING FINISHING] Specifically calibrated for DIY model post-processing and 3D printing deburring tool use. It effectively cleans up brims, rafts, support marks, and sharp edges from PLA, PETG, ABS, and resin prints. The compact 5.4 inch aluminum handle allows controlled pressure for plastic and resin part finishing without gouging delicate surfaces
- [MULTI-MATERIAL VERSATILITY] Engineered for deburring tool for metal, pipe reamer, pipe deburring tool, and burr removal applications on stainless steel, copper pipe, brass, aluminum, PVC pipe, sheet metal, and freshly cut parts. The kit includes a storage case for 10 spare deburring tool blades, making it a practical choice for machinists, plumbers, makers, and 3D printing hobbyists
- Workpiece material group and hardness
- Tool material, coating, geometry, and diameter
- Operation and toolpath
- Radial and axial engagement
- Machine and setup rigidity, including interrupted or unstable cutting
- Whether the figure is a minimum, starting recommendation, or maximum
If these conditions or the units differ, the numbers are not directly comparable. Manufacturer tables are recommendations with defined assumptions, not a guarantee that a given speed will produce a particular tool life or productivity outcome.
PC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchIs cutting speed the same as feed rate?
No. Vc is the relative surface speed at the cut; feed describes how quickly the tool advances through the work. Toolmaker charts list them separately—for example, Vc alongside feed per tooth for milling or feed per revolution for drilling and turning. A correct spindle speed does not determine the correct feed by itself.
Best Value

- EXTRA LARGE WOOD CNC ROUTER BIT: Shank: 1/4"; Cut Diameter:1-1/2"; Cut Length: 1/4"
- HIGH QUALITY CNC SURFACING ROUTER BIT: The sharp carbide tipped bit, solid hardened steel bodies with anti-kickback design. Build up with heat resistant Teflon coating which can reduce resin build-up for fast and easy cleaning. This CNC router bit is specifically designed and manufactured for the high quality demanded by woodworking industrial applications, BINSTAK router bit can withstand some heavy duty use and the test of time.
- VERSATILE ROUTING TOOl: This professional bottom cleaning router bit is not only perfect for wood slab flattening, resurface or plane the top surface of the spoilboard, but also for trimming and slotting/grooving. Great replacement bit tool for woodworking carpenter!
- USE RANGE for CNC ROUTING BITS: Suitable for solid woods, MDF, laminate, particle board, plywood compact panel, acrylic and etc. Avoid cutting metal and non-wood materials.
- Use on CNC and other automatic routers as well as hand-held and table-mounted portable routers. Such as woodworking engraving machine, trimming machine.
Engagement may call for separate adjustments to speed and feed. Use the guidance for the specific tool and operation instead of changing feed simply because Vc or rpm changed.
How should I handle unstable or interrupted cuts?
Cutting data commonly assumes particular conditions. Haas says the speed values in its indexable-drill guide are for stable conditions and recommends reducing its starting speed by 10% for unstable conditions and by 20% for interrupted cuts. These percentages are specific to that Haas guide; they are not universal adjustment rules for every tool or operation. Consult the applicable toolmaker guidance when the cut is unstable, interrupted, or otherwise differs from the chart’s assumptions.
Quick Recap
Quick checklist for selecting Vc
- Confirm the workpiece material group and condition.
- Use data for the exact tool family, grade, geometry, diameter, and operation.
- Convert Vc to rpm using the diameter at the cutting interface and consistent units.
- Check feed separately, along with engagement and stability guidance.
- Start from the maker’s stated recommendation, then assess the cut within tool and machine limits.
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.
Do these 3 things before closing this tab:
1Clear out junk files and repair common Windows errors2Fix the driver behind crashes, sound loss and screen glitches3Repair Windows errors before they cause bigger problems



