If an FDM print will not stick from its first lines, check the build surface, plate seating, first-layer setup, and filament profile. If the first layer holds but corners curl as the print grows, focus on cooling, drafts, material shrinkage, and contact area. Those symptoms can overlap, but they call for different fixes.
First, identify when the failure starts
Watch the skirt or the first lines around the model. If they fail to adhere immediately, start with surface cleanliness, plate seating, leveling or mesh calibration, nozzle-to-bed distance, extrusion, and the selected material profile. A skirt can expose a first-layer problem before the model itself is underway.
As an Amazon Associate I earn from qualifying purchases.
If the first layer is sound but corners lift several layers later, investigate shrinkage as the part cools, drafts, ambient temperature, model geometry, and whether the filament is prone to warping. A print can also have both problems: a marginal first layer leaves less grip to resist later contraction.
Clean and inspect the build plate
Remove stuck filament and debris, then clean grease from the surface using the plate maker’s instructions. Cleaning methods vary: Prusa recommends wiping relevant print surfaces with IPA 90% or higher, while UltiMaker’s S6 manual distinguishes between IPA for flexible plates and water, with detergent if needed, for glass. Do not assume that a solvent or adhesive suitable for one plate is safe for another.
#1 Best Overall

- WORKS ON MULTIPLE FILAMENTS: This versatile 3D printer glue is ideal for securing prints made with ABS, PLA, PETG, HIPS, and TPU filaments. This PLA glue's reliable bonding ensures your creations stay in place throughout all printing processes, making this adhesive glue an essential addition to your 3D printing supplies. Whether you are a professional or looking for gifts for 3D printer lovers, our adhesive glue guarantees smooth results across various filament types of all 3D printing projects. It is also compatible with TPU Flex filament.
- WORKS ON ALL SURFACES: Designed for flexibility, this 3D printer glue stick works seamlessly on different types of build surfaces like Flex Plate, Glass, PEI, Buildtak, Kapton, and more. The advanced formulation of this 3D printer adhesive glue ensures a secure grip on your 3D printer build plate for consistent and high-quality prints. Whether you are working with ABS glue or experimenting with different materials, this adhesive glue ensures reliable performance across every 3D printing surface.
- EASY TO USE: Applying this glue stick for 3D printing is effortless! Just shake, press, and apply to your active printing area. This 3D printer adhesive glue bonds seamlessly to the 3D printer build plate, reducing warping and delivering stable results. Compatible with various materials like PETG, it's the ultimate PETG glue for professional results. This 3D glue for 3D printing easily releases prints once cooled and cleans up with water, making our adhesive glue a staple for all 3D enthusiasts.
- LONG-LASTING ADHESIVE GLUE: Delivering over 100 prints, this 3D printer glue is built to last through multiple uses without reapplication. Perfect for all 3D printing materials, especially ABS, PLA, PETG, HIPS, and TPU filaments. It's the ultimate companion for hobbyists and professionals. This 3D adhesive glue provides ideal durability while remaining easy to apply. Whether using filament glue or other glue for 3D printing, it ensures strong bonds for consistent, high-quality prints every time. Magigoo MO2016 is also an essential addition to 3D printing accessories, supplies, and materials.
- ODOURLESS AND SAFE: This 3D printer adhesive glue is designed with your safety in mind. Completely odorless and non-flammable, this 3D printer glue is ideal for home, office, or educational settings, including workshops with kids. Whether you need a reliable adhesive glue for daily projects or a 3D printing adhesive for intricate designs, our adhesive glue delivers consistent results. Perfect for bonding ABS materials, this ABS plastic adhesive is a dependable choice for every printing hobbyist.
- Check that the sheet is flat, undamaged, and seated correctly.
- Look for trapped filament or debris beneath the sheet that could change its position.
- Clean both nozzle and plate before leveling or calibrating.
- Use glue only where the printer, plate, or filament manufacturer recommends it. UltiMaker advises applying glue as recommended and using it on a flexible plate only when specifically recommended for that material.
Prusa’s warping guidance and the UltiMaker S6 manual show why surface-care instructions should be matched to the particular build surface.
Correct the first layer without over-squishing it
Begin with the correct printer and filament profile, then check leveling or mesh calibration and first-layer height. The line should lie down evenly and bond to the surface, but pushing the nozzle too close is not a universal adhesion fix. Excessive squish can damage a sheet; Prusa specifically warns that lowering Live Adjust Z too far can damage its steel sheet.
Rank #2
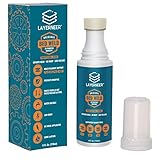
- THERMAL DYNAMIC COATING: Based on science, works like magic; Parts stick at hot and release when cooled; CHECK COMPATIBILITY IMAGE FOR YOUR SURFACE TYPE
- LONG LASTING: Print several times on a single coating; recharge with a wet sponge to get more prints out of a single application; Cost pennies per print
- LOW ODOR & WATER SOLUBLE: No harsh smells; No headaches; Easy to touch up or remove with water
- NO-MESS APPLICATOR: Built in foam tip makes applying the coating to your build plate surface simple and it won't accidentally spill
- WIDE FILAMENT COMPATIBILITY: Works with PLA, ABS, PETG, ASA, and CPE filaments for versatile 3D printing applications across multiple material types
Keep the profile’s nozzle and bed temperatures as your baseline. If adhesion remains poor, make gradual adjustments within the filament maker’s recommendations. In its first-layer guidance, Prusa says a 5–10 °C bed-temperature increase can be tried for experimental materials; that is not a universal instruction for every filament. Prusa also suggests trying about 75% print speed for the first three layers after other checks, a recommendation for its printers and workflow rather than a general speed rule.
See Prusa’s first-layer troubleshooting guide for its calibration and adjustment advice.
Rank #3
- 【Strong Adhesion】Liquid 3D printer glue is specially developed for 3D printing; it ensures consistent grip even during high-speed printing, prevents model lifting or warping, ensures a perfect first layer, and thereby increases printing success rates while reducing waste of filaments and time.
- 【Durable】The 3D Printer Glue provides strong bonding properties, requiring just a small amount per print. With 60ml, you can achieve lasting adhesion over many prints. For optimal results, it is recommended to reapply the glue before each printing session.
- 【Easy Print Release】Enjoy effortless removal of 3D prints after cooling, ensuring a hassle-free post-printing experience with 3D printer bed adhesive.
- 【Wide Compatibility】Ideal 3d printer bed adhesion solution for PLA, PETG, PET, ABS, ASA, and TPU. Adheres well to diverse 3D printing surfaces such as low-temperature, high-temperature, textured/smooth build plates, glass, PEI, PEO, PET, Buildtak, and aluminum plates,etc.
- 【Easy to Apply】Experience a mess-free process with Bamboo Lab 3D print glue. Simply press the applicator head to open the valve and spread evenly over the printing area. Its liquid form ensures a more uniform and quicker application compared to solid 3d printer glue stick for hot bed.
Add first-layer contact area for small bases and lifting corners
A brim adds a flat border around the model, increasing the area that touches the plate. It is a practical next step for a tall object with a small footprint, several small parts, or corners that begin lifting. Prusa’s brim guide generally advises a width of at least 3 mm; the useful width still depends on the model and slicer. A brim may need trimming after printing.
For an isolated problem corner, Prusa also suggests adding a small sacrificial geometry nearby. A skirt or draft shield can help retain heat around parts made from higher-warp materials. These slicer options are worth considering before adding surface treatments; glue may require cleanup and can affect how readily a print releases.
Rank #4

- Quality Assurance: Produced by Creality, our 3D printer glue sticks guarantee reliability and consistent performance
- Eco-friendly Composition: Formulated from PVP material without the addition of formaldehyde, these 3D printer glue sticks prioritize safety and environmental sustainability, providing a safer and healthier printing environment
- Premium 3d Printer Adhesive: Engineered specifically to elevate the 3D printing process, they facilitate smooth application for thin coatings, ensuring precise prints with improved adhesion at high temperatures and easy demolding post-cooling
- Easy Maintenance: Designed for simple upkeep, they are water washable, enabling the printing glue easily cleaned without leaving any residue behind
- Wide Compatibility: With versatile adaptability, these 3D print glue sticks effectively adhere to various materials and printing bed surfaces, ensuring compatibility across diverse printing setups
Details are in Prusa’s skirt and brim guide and warping guidance.
Match cooling and enclosure choices to the filament
Plastic contracts as it cools. With higher-temperature materials such as ABS, ASA, and PC, the temperature difference between the hot part and surrounding air can create stress that pulls corners upward. Reduce drafts and keep the ambient temperature stable; consider an enclosure for materials that need one.
Best Value

- Quality Assurance: Produced by Creality, our 3D printer glue sticks guarantee reliability and consistent performance
- Eco-friendly Composition: Formulated from PVP material without the addition of formaldehyde, these 3D printer glue sticks prioritize safety and environmental sustainability, providing a safer and healthier printing environment
- Premium 3d Printer Adhesive: Engineered specifically to elevate the 3D printing process, they facilitate smooth application for thin coatings, ensuring precise prints with improved adhesion at high temperatures and easy demolding post-cooling
- Easy Maintenance: Designed for simple upkeep, they are water washable, enabling the printing glue easily cleaned without leaving any residue behind
- Wide Compatibility: With versatile adaptability, these 3D print glue sticks effectively adhere to various materials and printing bed surfaces, ensuring compatibility across diverse printing setups
Cooling is not simply a matter of turning the fan off. Prusa advises checking that part cooling is operating for materials such as PLA and PETG. For some small or overhung regions in enclosed, high-temperature prints, low fan levels may help, but too much cooling can lift a print or weaken layer-to-layer bonding. If added cooling is followed by cracking or poor bonding between layers, Prusa suggests raising nozzle temperature enough to restore bonding, within the material’s guidance.
An enclosure is not a universal cure. Prusa says one may be needed for ASA, ABS, PC, PA, PP, and related composites; PLA and PETG generally need more cooling, which can be harder to provide in a warm enclosure. Check your printer’s and filament’s instructions before changing the environment. Prusa explains the material trade-offs in its enclosure guide and warping article.
Use temperature recommendations only within their stated scope
Temperature values belong to specific filament profiles and setups, not to all printers using a material with the same name. For example, Prusa’s ASA guidance lists a 260 °C nozzle temperature and a bed temperature of 105 °C for the first layer and 110 °C for subsequent layers. It also recommends a glue stick on the specified smooth or powder-coated PEI sheets. Treat these as Prusa’s ASA recommendations for the surfaces it names, not universal ASA settings or permission to apply glue to any plate.
Recommended Free Tools
Check the filament and printer maker’s settings before changing temperatures or surface treatments. Prusa’s ASA guide gives the context for its values and plate advice.
Quick Recap
Choose the next fix by symptom and compatibility
| What you observe | What to check or try next | Important constraint |
|---|---|---|
| First lines or skirt fail immediately | Clean and inspect the plate; confirm it is seated; check leveling, first-layer height, extrusion, and the material profile. | Use cleaning products and surface treatments approved for that specific plate. |
| First layer holds, then corners lift | Reduce drafts, stabilize ambient conditions, add a brim, and review cooling and material choice. | Cooling and enclosure needs depend on the filament. |
| A tall or small-footprint model loses grip | Try a brim to enlarge the first-layer contact area. | A brim is easy to test but may need trimming. |
| A high-warp material lifts or cracks | Review enclosure, fan, and nozzle settings against the material guidance. | Too much cooling can cause lifting or poor layer bonding; a warm enclosure may not suit PLA or PETG. |
| Adhesion remains inconsistent after surface checks | Recheck first-layer calibration and the selected printer/filament profile before making gradual changes. | Do not compensate automatically by forcing the nozzle closer. |
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.




