Quick wins for a faster PC:
Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Repair Windows errors before they cause bigger problemsFix Now →Use traditional automation for actions you can specify precisely; use industrial AI for patterns, predictions and recommendations that fixed rules cannot capture. A programmable controller, safety system or manufacturing execution system (MES) should continue to run the functions it was engineered and validated to perform. AI is most useful alongside those systems when operational data can support condition forecasts, anomaly detection, quality analysis, scheduling help or process optimization. In practice, the strongest design is often hybrid: deterministic controls execute the approved response while an AI layer supplies earlier warnings or better decisions.
The choice is not a contest between an old technology and a new one. It is an engineering decision based on task clarity, consequences of error, data quality, integration effort, explainability, human oversight and measurable business outcomes.

As an Amazon Associate I earn from qualifying purchases.
What industrial AI and traditional automation actually do
Traditional automation turns an understood process into repeatable logic. Engineers define sequences, limits, interlocks, setpoints and exception handling; controllers and operational software execute them consistently. The approach is well suited to machine sequencing, keeping a process within an established range, tracking material and enforcing known production rules.
Industrial AI uses data to estimate, classify, detect, predict or recommend. A model may learn that a combination of vibration, temperature and pressure readings tends to precede a failure, or that certain process conditions correlate with a quality defect. It can surface a pattern that would be difficult to express as a short list of fixed rules. It does not, by itself, know whether a suggested action is safe, permitted or practical on a particular line.
#1 Best Overall

- INDUSTRIAL VIBRATION METER – VM-424 WITH REMOTE SENSOR PROBE - Designed for vibration measurement on motors, pumps, compressors, gearboxes, fans and rotating machinery where direct placement of a handheld meter is difficult. The external sensor allows technicians to reach narrow measurement points while keeping the main unit at a safe and comfortable viewing position.
- 3-IN-1 VIBRATION MEASUREMENT – ACCELERATION VELOCITY DISPLACEMENT - Measures Acceleration 0.1–199.9 m/s² (peak), Velocity 0.1–199.9 mm/s (RMS) and Displacement 0.001–1.999 mm (p-p), enabling technicians to evaluate key vibration parameters used in machine condition monitoring and preventive maintenance inspections.
- DUAL FREQUENCY ACCELERATION MODES – 10HZ–1KHZ AND 1KHZ–3KHZ - Low frequency mode supports general machine vibration evaluation such as imbalance or structural vibration, while high frequency mode helps observe higher-frequency vibration components during mechanical diagnostics.
- REMOTE PIEZOELECTRIC SENSOR – STABLE CONTACT MEASUREMENT - External shear-type accelerometer connected by cable allows precise probe positioning on bearing housings, pump casings and motor frames while the display remains easy to read during measurement.
- INTERCHANGEABLE PROBE TIPS – MAGNETIC, SHORT AND LONG CONTACT - Includes magnetic base tip for hands-free contact on metal surfaces as well as short and long probe tips for measurements on flat surfaces, narrow housings and recessed machine components.
NIST defines industrial artificial intelligence in system-specific terms: “Industrial Artificial Intelligence (IAI), or Artificial Intelligence applied to industry applications, is defined by its requirement to fulfill an explicit need of a system, while both utilizing and being bounded by the limitations and capabilities of that system.” In other words, an impressive model in isolation is not enough. Its usefulness depends on the machine, process, people, data and operating constraints around it.
| Decision axis | Traditional automation | Industrial AI |
|---|---|---|
| Primary job | Execute specified sequences, rules and control logic | Find patterns in data; estimate, classify, predict or recommend |
| Best conditions | Stable, understood tasks where repeatability and predictable response matter | Complex or changing processes where useful signals exist and outcomes can be measured |
| Typical applications | Machine sequencing, interlocks, setpoint control, standard workflows and material tracking | Condition monitoring, predictive maintenance, visual quality inspection, anomaly detection, scheduling support and optimization |
| How it changes | Through engineering, configuration, commissioning or revised rules | Through model training, evaluation, versioning, monitoring and maintenance |
| Critical dependencies | Correct specifications, sensors, control design and maintenance | Representative contextual data, model fitness, integration, monitoring, explainability and a defined human process |
This comparison is a practical synthesis, not a claim that every controller is perfectly deterministic or that every AI model improves automatically. The responsible controls and safety engineers must decide which functions can be automated and how they will be validated.
When conventional automation is the better choice
The operation has a clear specification
If the desired behavior can be written as a sequence, limit, interlock or state transition, conventional control is usually the sound starting point. Examples include opening valves in a known order, stopping a motor when a guard is opened, holding temperature inside an established range, or rejecting a part when a measured dimension is outside its specification. The rule is visible, testable and directly tied to the process requirement.
PC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchA predictable response is more important than pattern discovery
Safety functions, emergency stops and protective interlocks require known behavior under defined conditions. An AI score can inform a separate decision, but it should not silently replace a validated safety function. If a missed event could injure someone, damage equipment or create a hazardous release, the control and safety architecture needs explicit engineering approval, testing and documented responsibility.
The process is repetitive and stable
Automation delivers value without a large historical data set when the work is already understood. A controller can repeat a recipe, coordinate robots, enforce timing and log results from the first commissioned cycle. Adding a model to a stable task may increase complexity without improving the result.
The plant needs execution structure
An MES and related operational software organize production orders, work instructions, machine states, material genealogy, quality records and operator actions. A vendor description from Rockwell Automation Plex characterizes MES as connecting people, processes, machines and data, while positioning AI as an analysis and prediction layer over that context. AI does not automatically provide the transaction records, permissions, workflow controls or audit trail that an MES is designed to provide.
Rank #2
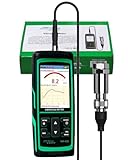
- PROFESSIONAL VIBRATION ANALYZER – VM-428 WITH EXTERNAL SENSOR - Designed for advanced vibration diagnostics on motors, turbines, pumps, compressors and rotating machinery where higher measurement ranges and additional diagnostic parameters are required.
- 5-PARAMETER MACHINE DIAGNOSTICS – A V D FREQUENCY TEMPERATURE - Measures Acceleration 0.1–300 m/s² (peak), Velocity 1–850 mm/s (RMS), Displacement 1–3300 µm (p-p), Frequency 30Hz–14kHz and Temperature, providing multiple diagnostic indicators for machine condition evaluation.
- DUAL FREQUENCY MEASUREMENT CIRCUIT – STRUCTURAL AND HIGH-FREQUENCY MODES - Low frequency mode supports general vibration analysis of machine structures, while high frequency mode allows observation of higher-frequency vibration signals often associated with mechanical wear or bearing conditions.
- REMOTE MAGNETIC SENSOR – STABLE AND REPEATABLE MEASUREMENTS - External piezoelectric shear-type probe with magnetic base allows secure placement on metal housings, supporting stable readings during inspection of motors, gearboxes and rotating equipment.
- ISO MACHINE CONDITION RATING INDICATION - Built-in vibration severity scale based on ISO vibration classification helps technicians visually interpret measured velocity levels during machine condition evaluation.
- Choose conventional automation first when the sequence and acceptance criteria are known.
- Keep deterministic logic for interlocks, limits and responses that must be proven before operation.
- Use engineering changes and formal commissioning when the process specification changes.
- Do not add AI merely because a system has data; add it when a defined decision is otherwise difficult to make.
When industrial AI can add value
Predictive maintenance and condition monitoring
NIST identifies temperature, vibration and pressure as examples of signals that can support predictive maintenance. A model can estimate that a bearing, spindle or pump is moving toward an abnormal condition, allowing a planner to inspect it during a scheduled stop rather than after an unplanned failure. The useful output is not a generic “maintenance score”; it is an actionable alert linked to an asset, time horizon, likely condition and an approved response.
Recommended Free Tools
A category such as an industrial vibration sensor can be part of the measurement system, but a sensor alone is not an AI system. Before buying or installing one, verify that its range, sampling, mounting, environmental rating and synchronization fit the machine and that the resulting data can be connected to the historian, control network or maintenance workflow.
Anomaly and quality detection
Rules work well for a known out-of-limit value. AI may help when defects arise from combinations of variables, subtle visual features or changing operating conditions. A model can flag an unusual waveform, image or process signature for review and help rank likely causes. It still needs representative examples of normal and abnormal production, a way to handle unknown conditions and a human process for dispositioning a suspect part.
Scheduling and bottleneck reduction
NIST’s manufacturing AI work includes production scheduling and system integration as case-study areas. Scheduling assistance can evaluate many constraints—orders, due dates, changeovers, material availability, machine capacity and maintenance windows—when a fixed priority rule produces frequent bottlenecks. The planner should be able to inspect assumptions, approve a proposed sequence and override it when conditions on the floor differ from the data.
Process optimization
NIST’s implementation guidance cites optimizing cycle time, reducing bottlenecks and reducing repetitive work as possible targets. An optimization model is appropriate when there is a measurable objective and enough operating range to learn from, such as reducing energy per unit while preserving quality. Define the allowed operating envelope first; a recommendation that improves one metric by violating a quality, safety or equipment constraint is not an improvement.
Tasks with changing or hard-to-specify patterns
AI becomes more attractive when the process is affected by interactions that are difficult to enumerate in rules, yet the plant can collect contextual data and measure outcomes. Examples include gradual tool wear, product-mix effects, variable raw material behavior and interactions among several machine states. The model must be evaluated on conditions it did not simply memorize from training.
Rank #3

- 【5-in-1 Diagnosis】The vibration meter supports measurements of Acceleration 0.1–300 m/s² (peak), Velocity 1–850 mm/s (RMS), Displacement 1–3300 µm, Frequency 30 Hz–14 kHz, Temperature 14~140°F. The vibrometer gauge meets the common predictive maintenance and condition check needs in workshops and production sites.
- 【Wide Range of Applications】This digital vibration analyzer is suitable for motors, HVAC systems, pumps, fans, generators, compressors, turbines, bearings, etc. The tester features ISO vibration intensity classification. You can quickly get a preliminary assessment of machine/vehicle vibration. Appropriate for mechanical maintenance technicians, engineers, QC inspectors, or even beginners.
- 【Large Storage & Transmission】This vibration meter supports automatic/manual recording (stores up to 8 MB ≈397,000 data points). It can transfer CSV and BMP files via PC software (compatible with Windows systems) or be used as a small-capacity USB drive. Handy for long-term trend analysis and batch data archiving of equipment records.
- 【Clear Display & Stable Measurement】The easy-to-read backlit screen enables data collection and interpretation under various lighting conditions. It clearly shows line graphs and real-time statistics of maximum/minimum/average values. The separate probe comes with a strong magnetic sensor, which helps access hard-to-reach areas and minimizes the impact of your movements on the results.
- 【User-friendly Design】The vibration detector comes with a portable carrying case for outdoor use. It supports automatic high/low-speed circuit switching, adjustable sampling time, screen brightness, calibration, unit switching, automatic power-off, machine-grade selection, low battery indicator. The included manual provides a detailed explanation of each function. Setup takes only a few seconds.
Why a hybrid architecture is common
A practical plant architecture gives each layer a distinct responsibility:
- Control and safety layer: PLCs, safety systems and other validated controls execute sequences, interlocks and approved setpoints.
- Execution and context layer: MES, historians and maintenance systems record orders, states, genealogy, work instructions and events.
- AI analysis layer: Models detect anomalies, forecast conditions, classify quality signals or propose schedules using contextualized data.
- Decision layer: An operator, planner, engineer or a separately validated procedure reviews the output and chooses the permitted action.
For example, an AI model can identify a rising probability of spindle wear, attach the relevant vibration trend and recommend an inspection. The maintenance workflow then creates a work order, while the controller continues to run the machine under its existing limits. Whether an AI output may directly alter a control loop is a separate safety and validation decision; an AI recommendation is not evidence that a control action is safe.
NIST’s Industrial AI Assessment and Measurement Methodology emphasizes that assessment must account for system limitations and impacts on users. Its work on decision-making, planning and control therefore points toward procedures that specify who reviews an output, what evidence is required, what actions are allowed and how an override is recorded.
The Tool Desk
Outbyte PC Repair FREERepair Windows errors before they cause bigger problemsFix Now →Outbyte Driver Updater FREEScan for outdated or missing drivers - takes under a minuteDriver Scan →A decision framework for choosing the right approach
Evaluate the problem and its operating constraints before selecting a technology. The following questions turn a broad AI-versus-automation debate into an engineering decision.
| Question | If the answer points to conventional automation | If the answer supports an AI pilot |
|---|---|---|
| Can the desired behavior be expressed as a stable rule or sequence? | Implement and validate the rule in the control or execution system. | Look for interactions, gradual changes or patterns that rules cannot capture. |
| How severe is an error? | Keep high-consequence actions in validated control and safety functions. | Use staged recommendations, independent checks and explicit human approval. |
| Are the relevant data available and trustworthy? | Proceed with specified sensors and normal commissioning. | Check coverage, timestamps, labels, missing values, machine identity and operating context before modeling. |
| Will the result fit existing systems and work? | Use the established interface and workflow. | Budget for historians, MES, maintenance, identity, network and notification integration; test semantic correctness, not just connectivity. |
| Can a user understand and trace the output? | Document the rule, revision and test results. | Record model version, input data, threshold, explanation, decision and override. |
| What outcome will prove value? | Measure response time, repeatability, compliance or commissioning performance. | Set a baseline and target for downtime, quality, yield, throughput, cycle time, maintenance workload or false alarms. |
NIST’s 2026 Roadmap on Artificial Intelligence and Machine Learning for Smart Manufacturing, published July 3, 2026, identifies industrial big data, data management, integration with heterogeneous sensing and control systems, and trustworthy, explainable and reliable operation in high-stakes environments as continuing deployment challenges. Those are decision criteria, not reasons to buy a particular product.
How to implement industrial AI without losing operational control
1. Define one decision and one measurable outcome
Start with a specific question: “Should this pump be inspected during the next planned stop?” is actionable; “How can we use AI in the plant?” is not. Establish the current baseline, the target, the time window and the person who can act on an alert. Include the cost of false positives, missed events and delayed decisions in the evaluation.
Rank #4

- 【Integrated Vibration Sensor】Real-time capture of 3-axis vibration and temperature data: Vibration displacement (0~30000um) + Speed (0~50mm/s) + Amplitude (0~180°) + Operating temperature (-20°C~60°C). Vibration and shock omnidirectional measurements can prevent breakdowns and repair costs.
- 【BLE 5.0 Low Power】 50m transmission distance, approximately 8 hours battery life. Bluetooth 5.0 is compatible with Android/iOS systems. The WITMOTION APP supports connecting sensors on smartphones (up to 4 on the same phone). It can also be connected to a computer via TYPE-C, making it easy for users to choose the best connection.
- 【Easy Install & Use】The wireless design allows the sensors to be installed on machine parts that are difficult to access. A small and portable sensor designed with strap holes at both ends that can be used and go anywhere.
- 【Analysis Vibration Sensor System】Condition monitoring and vibration analysis are seamlessly integrated with WITMOTION PC software, making it quick and easy to analyze and visualize data. Maintenance teams can set it up as needed.
- 【Attitude Measurement More Accurate & Reliable】Sensors integrated R&D fusion algorithm, low noise level, and increasing measurement accuracy ensuring stable data output. WITMOTION has been focusing on the sensor field for 10 years, providing professional attitude measurement solutions globally.
2. Map the existing control and information flow
Document which PLCs, safety systems, historians, MES modules, quality systems and maintenance tools own each signal and action. Identify read-only interfaces first. Do not bypass an interlock or write to a controller simply to make a pilot appear integrated.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
3. Audit the data before training a model
Check whether measurements are synchronized, calibrated and labeled with the machine, product, recipe, tool, operator shift and maintenance state that give them meaning. Look for missing periods, sensor changes, inconsistent units, unrecorded manual interventions and too few examples of the event you want to detect. Separate training, validation and test periods by time or operating condition so that the evaluation reflects deployment.
4. Confirm that the signal can be measured in production
Data collection is an engineering problem, not a spreadsheet task. NIST’s AIMS project notes that force and vibration signals useful for machine-tool monitoring may not be practically measurable in production without suitable methods. Mounting, cabling, sampling, electromagnetic noise, access and maintenance all affect the signal. Solve those constraints before promising model accuracy.
5. Run a bounded, shadow-mode pilot
Begin with recommendations or alerts that do not change the process automatically. Compare predictions with actual failures, inspections or quality outcomes. Record false alarms, missed events, latency and the time operators need to investigate. A pilot should have a stop condition and an owner who can disable it without affecting the validated control path.
6. Validate with domain experts
Controls, process, quality, maintenance, safety and production users should review representative cases, edge cases and failure modes. Test semantic correctness: does “high vibration” refer to the intended axis, asset and operating state? NIST’s manufacturing AI work proposes comparing manual standards-based, AI-generated and hybrid integration approaches using effort, performance, semantic correctness and scalability.
7. Define the operating procedure
Write who receives an alert, how quickly it must be reviewed, what evidence is checked, which actions are allowed, when escalation occurs and how an override is logged. Explainability is useful only when it helps a person make and document a better decision.
Best Value
8. Monitor after deployment
Track data quality, model performance, alert volume, drift, latency and business outcomes. Recheck the model after a machine rebuild, sensor replacement, tooling change, product change or process redesign. Version the model and its data pipeline, and preserve enough information to reconstruct why a recommendation was made.
Independent reader supportYour contribution helps us test, update, and keep practical guides available for everyone.Risks and common failure modes
Assuming a generic model fits every machine
NIST’s AIMS project warns that pretrained generic tools may not be accurate for a specific machine. Machine-specific measurement, periodic verification and model updating may be necessary. A model that performs well on one spindle, press or pump should not be transferred to another asset without evidence.
Collecting data without context
A timestamped sensor stream cannot explain itself. Product type, recipe, tool, speed, load, maintenance state and environmental conditions can change the meaning of the same value. Without that context, a model may learn the shift, product mix or sensor replacement instead of the condition you care about.
Do these 3 things before closing this tab:
1Repair Windows errors before they cause bigger problems2Scan for outdated or missing drivers - takes under a minute3Clear out junk files and repair common Windows errorsOptimizing the wrong metric
A system tuned only for fewer alerts may miss defects. A system tuned only for sensitivity may overwhelm operators with false alarms. Pair every technical metric with an operational measure, such as verified downtime avoided, accepted quality, planner hours saved or maintenance work completed at the right time.
Treating connectivity as integration
Publishing a data stream is not the same as fitting a plant workflow. Names, units, asset hierarchies, permissions, timing and failure handling must agree across systems. Compare integration methods on effort, performance, semantic correctness and scalability rather than assuming that an API connection solves the problem.
Ignoring interpretability and traceability
Users need to know which asset and period generated an alert, what model version ran, which inputs mattered and what threshold was applied. Keep an audit trail for decisions and overrides. In high-stakes settings, domain-specific testing and evaluation are more useful than a generic accuracy number.
Promising savings before establishing a baseline
The available guidance describes potential applications, not a universal return on investment or a general percentage improvement over conventional automation. Measure the current process first, then compare the AI-assisted process against that baseline under similar production conditions.
Free tools Windows power users keep installed
One-click scans. No signup required.
Examples of matching the tool to the problem
| Plant situation | Recommended starting point | Reason |
|---|---|---|
| A guarded conveyor must stop when a gate opens. | Validated safety and control logic. | The condition and response are explicit, and predictable behavior is essential. |
| A filling machine follows a fixed recipe with known limits. | PLC/MES sequence and limit checks; add AI only for a defined secondary problem. | Execution, traceability and repeatability are already specified. |
| A spindle gradually changes behavior before an unplanned failure. | Hybrid condition monitoring: sensors and AI alerting above the existing control layer. | Multivariable trends may be difficult to encode as fixed rules, while the machine still needs its validated controls. |
| Defects depend on subtle image and process combinations. | AI-assisted inspection with human disposition and established quality records. | A model can detect complex visual patterns, but release decisions require context and traceability. |
| Many orders compete for machines with changeover and maintenance constraints. | AI scheduling support with planner approval and MES execution. | The model can evaluate combinations; the execution system remains the system of record. |
| A process has no reliable sensors or outcome labels. | Fix instrumentation, data definitions and operating procedures first. | Model training cannot compensate for unmeasured conditions or ambiguous outcomes. |
How to make the final choice
Choose traditional automation when the task is specified, repeatable and safety- or compliance-sensitive, and when a rule can deliver the required result. Choose industrial AI when a measurable decision depends on patterns that are difficult to encode, the plant can collect representative contextual data and users have a defined way to act on the output. Choose a hybrid when control and execution need deterministic behavior but maintenance, quality, scheduling or optimization can benefit from prediction.
- Write the decision and permitted action before selecting a model.
- Keep safety functions and validated interlocks in the architecture designed for them.
- Prove that measurements are available, contextual and maintainable in production.
- Start with a bounded pilot and compare against a documented baseline.
- Require traceability, human oversight and a rollback path before expanding scope.
- Revalidate after changes to machines, sensors, products, recipes or workflows.
The technology is successful when it improves a defined operational outcome without weakening control, safety or accountability. Novelty is not a selection criterion; fit to the system is.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

