Quick wins for a faster PC:
Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Repair Windows errors before they cause bigger problemsFix Now →Scan for outdated or missing drivers - takes under a minuteDriver Scan →An AI-enabled automotive smart factory is not created by adding a model to a production line. It depends on a reliable path from machine signals to production context and then to a decision people or systems can act on. That path connects controls and sensors, gateways, interoperable data, manufacturing operations and enterprise systems, and finally analytics or AI. Start with a costly or time-sensitive production decision; then build and measure the data flow needed to improve it.
What makes an automotive factory smart?
A smart factory is an integrated data and decision environment. A machine value becomes useful when the plant can associate it with the right asset, process, product, order, shift, and time—and present it to someone or something able to respond.
As an Amazon Associate I earn from qualifying purchases.
NIST’s smart-manufacturing architecture connects field devices and gateways with controls, manufacturing operations management (MOM), enterprise resource planning (ERP), cloud computing, and AI services. The architecture is a way to think about connected functions, not a requirement that every plant use one product or move every signal to the cloud.
For example, a press cycle count on its own says little about whether the line is meeting the current order. Joined to a line identifier, product, target rate, and production schedule, it can help operations identify a shortfall. A temperature reading may be useful for equipment monitoring, but for a quality decision it needs the relevant process step, product or batch, limits, and timing. Those links depend on plant data and system integration, not on AI alone.
#1 Best Overall

- Multi-Protocol Support: Integrates with industrial systems and supports multiple communication protocols, including Modbus RTU/TCP, BACnet, OPC UA, OPC XML-DA, and IEC 104, enabling seamless connection with diverse industrial devices to meet different automation needs.
- Cloud Data Connectivity: Functions as an MQTT, HTTP, and Socket client, providing reliable data transmission and automatic reconnection to maintain continuous data flow for IoT applications.
- JS Script Programming Support: Offers flexibility through JavaScript scripting, allowing users to customize and extend the gateway's capabilities to meet specific application needs.
- Alarm and Event Management: Allows users to set trigger conditions, enabling event triggers and releases based on state transitions.
- Easy Configuration and Management: User-friendly graphical configuration software simplifies setup, allowing easy access to real-time and historical data through an HTTP server interface.
How shop-floor signals become actionable information
The practical data path has several layers. Existing plants may combine old and new equipment, so the design must account for what each machine can expose and which systems already hold production information.
| Layer | What it contributes | What to verify |
|---|---|---|
| Machines, controls, sensors, and field devices | Signals such as machine state, cycle events, process measurements, and resource use. | Which signals are available, how they are encoded, their quality, and whether collection can be added without disrupting production. |
| Adapters and edge gateways | Collect and communicate data from equipment to other plant systems; gateways can help connect legacy equipment. | Compatibility with installed controls and interfaces, reliable operation, security requirements, and the timing the use case needs. |
| Industrial interfaces and data models | Provide ways to exchange and organize information across equipment and applications. | Whether the interface is supported by the installed equipment and whether the data carries consistent meaning, not just a readable value. |
| MOM and enterprise systems | Connect machine events with production operations and business context, such as schedules, orders, and quality or maintenance records. | How identifiers and timestamps match across systems, and which system is authoritative for each piece of context. |
| Analytics, AI, and operator workflows | Turn contextualized information into a forecast, alert, recommendation, or automated response. | Whether the output is timely and understandable, who owns the response, and how the result will be evaluated against a baseline. |
This is a logical flow, not necessarily a one-way chain. A decision may prompt an operator to update a work process or a control system to take an approved action. Define that response path explicitly; a dashboard that identifies a problem but leaves ownership unclear has not completed the operational loop.
Choose interfaces for the equipment and the job
Interoperability is foundational, but adopting a named standard does not by itself make data consistent. NIST’s technical discussion identifies MTConnect and OPC UA among standards used to harmonize shop-floor data exchange and notes that existing field standards are not interchangeable. It also places standards such as ISA-95/IEC 62264 and QIF at higher manufacturing layers and discusses MQTT among IIoT connectivity options.
Recommended Free Tools
Rank #2

- Multiple Internet access methods is offered: Global frequency LTE 4G/3G & Ethernet port & ADSL.
- Router fucntion is supported: Routing, VPN and firewall.
- Super Powerful Edge Computing Capabilities
- Support graphical programming (Node-RED) to quickly develop edge computing functions to meet unique functional requirements.
- Suitable for a variety of industrial IoT scenarios, supporting Modbus RTU/TCP protocol conversion and other popular PLC common protocols.
| Standard or option | Where it appears in NIST’s discussion | Decision to make |
|---|---|---|
| MTConnect | Shop-floor data harmonization and field/control options. | Check whether the equipment and applications in scope support it and whether the information it exposes suits the intended use. |
| OPC UA | Shop-floor data harmonization and field/control options. | Check device and system support, the required exchange pattern, security needs, and how data meaning will be aligned. |
| MQTT | Discussed as an IIoT connectivity choice. | Assess its fit for the plant’s connectivity and integration constraints; connectivity alone does not establish shared production semantics. |
| ISA-95/IEC 62264 and QIF | Shown among standards at higher manufacturing layers. | Assess whether they support the information exchange and system boundaries involved in the use case. |
These options address different interface and information-exchange problems; they are not a pick-one ranking. Compare them against the installed machine and control base, vendor support, data meaning, timing and reliability needs, cybersecurity requirements, and integration effort across OT, MOM, and enterprise systems. Check current editions and support with the relevant standards bodies and suppliers before committing to an implementation.
Start with a production decision, not an AI model
A focused first use case makes it easier to tell whether the data is adequate and whether the result helps the people running the plant. Select a decision whose delay or inconsistency has a visible operational cost, such as when to investigate an equipment condition, how to respond to a process deviation, or where a production constraint is developing. Treat these as candidate use cases, not guaranteed AI applications: the right solution may be a better connection, a clear rule, or an operator-facing trend rather than a predictive model.
- Define the decision. Specify who needs to decide what, when the decision is needed, and what outcome would count as improvement.
- Map the information sources. Identify relevant machines, controls, sensors, gateways, MOM or ERP records, and existing quality or maintenance data. Record who owns each system and signal.
- Check connectivity and data quality. Confirm that the needed signals can be collected consistently. Examine missing or late values, inconsistent units, duplicate events, clock alignment, and changes in machine or product identifiers.
- Define shared context. Agree how the plant identifies assets, lines, products, orders, process steps, and timestamps across systems. Decide which application owns each identifier and how changes are managed.
- Connect through supported interfaces. Test the chosen adapters, gateways, and standards with the actual equipment and systems in scope. Verify that the exchanged values retain their intended meaning.
- Establish a baseline. Measure current performance using a defined period and method before introducing a recommendation or alert. Choose metrics tied to the original decision, such as response time, quality, uptime, or output.
- Test the operator workflow. Put the output in front of the people expected to use it. Make the recommended action, supporting information, and escalation path clear; record whether the signal was useful and what happened next.
- Evaluate and scale selectively. Review operational value alongside reliability, safety, quality, cybersecurity, support burden, and integration effort. Expand only where measured value persists under the conditions of the next line or plant.
This sequence is a practical synthesis of NIST use-case guidance and manufacturing case examples, not a universal prescribed standard. A pilot establishes whether a scoped approach works under its test conditions; it does not by itself establish plant-wide readiness.
Rank #3
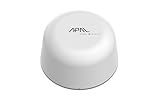
- SATELLITE CONNECTIVITY WHERE OTHERS FAIL: Eliminate dead zones in Agriculture, Forestry, and Mining. Unlike standard LoRaWAN or Cellular networks that require nearby gateways, the Hestia A1 connects directly to the 3GPP NTN Satellite network for deep mountains or open oceans where terrestrial signals cannot reach
- MODBUS PROTOCOL COMPATIBILITY: Built as Modbus Slave Device, Hestia can be connected to most Modbus IoT Host systems to enable satellite connectivity for industrial applications
- PLUG-AND-PLAY VIA RS485/MODBUS: Simple Python script integration with Python samples for Modbus/MQTT available on GitHub. Open custom code architecture provides flexibility for developers without black box limitations
- INCLUDES 3-MONTH SATELLITE DATA PLAN (30KB): Start your remote monitoring project immediately with a free 30KB / 3-Month satellite data plan via the CeresGate platform (Email registration required). Comes with Python sample code on GitHub for easy integration with Raspberry Pi, Linux, and Modbus devices
- TWO-WAY SATELLITE COMMUNICATION & CONTROL: Supports bidirectional data transmission allowing you to receive telemetry from remote sensors and send commands back to control equipment such as opening valves or resetting devices from the cloud without needing complex LoRaWAN infrastructure
Where digital twins and AI fit
A digital twin is a scoped implementation approach, not automatically a complete virtual replica of a factory. NIST’s 2021 publication on ISO 23247 presents manufacturing use-case scenarios that can help frame a twin around a particular asset, process, or production decision. Define what physical system the twin represents, which data keeps it connected to that system, and what decision it is meant to support.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
A NIST-indexed 2020 conference case study describes a digital twin for a manual manufacturing process that combined physical-world data with simulation and reinforcement learning for shop-floor decision-making and production-output prediction. Its abstract also cautioned that methods then available for predicting human engagement in smart manufacturing were insufficient for real-time activities. The case illustrates a research approach; it does not establish current capabilities or prove that the approach is suitable for an automotive production line.
AI belongs downstream of dependable capture and context. Depending on the use case, analytics may flag unusual behavior, estimate a future condition, or recommend a response. Before using a model operationally, establish how its inputs are maintained, how its output is checked, who can override it, and what happens when data is missing or the recommendation conflicts with established process controls. Keep safety-critical controls and production authority within the plant’s approved engineering and governance boundaries.
Rank #4

- 【Built-in 4G LTE Module】 With a standard SIM card slot that supports the 4G LTE network. It can move into 4G LTE wireless network if the Ethernet Internet fails, in order to ensure constant data transmission in the critical facilities. (Not support Verizon Network in the US)
- 【Industrial Hardware】 Qualcomm QCA9531 chipset provides stable performance, it is commonly used within the industry, which is perfect for industrial users to avoid breakdown. The Built-in hardware watchdog ensures the stability. It’s dedicated hardware that can detect and trigger a processor reset if necessary.
- 【Open Source & Secure】 OpenWrt pre-installed. Perfect for developers or IoT integration development. It supports 30+ VPN service providers, including OpenVPN & WireGuard.
- 【Compact Design】 Its aluminum alloy shell, optional wall-mounted design, and wide range of operating temperature are designed for easy installation, storage, and operation in tough industrial environments.
- 【Easy Configuration】 Supports AT command, manual/automatic dial number, and signal strength checking in our new admin panel for better management and configuration.
What manufacturing case studies do—and do not—show
Published examples can show how integration or task-focused automation was implemented, but their results should not be treated as expected savings for another plant. The settings, processes, and technologies differ.
| Example | Reported result or implementation | How to interpret it |
|---|---|---|
| Magellan Aerospace, NIST MEP case, 2022 | The aerospace operation in Middletown used Siemens Teamcenter and SFC for engineering and work instructions, plus an MTConnect implementation monitoring more than 40 devices, including CNC equipment, furnaces, power quality, and argon consumption. Encrypted data acquisition, SmartBox hardware, and an IIoT platform supported real-time status, utilization, and efficiency monitoring. The case reports a 1.4% reduction in shop rate tied to $51,473 in scrap and rework cost reduction; a 2.1% efficiency increase associated with $135,900 in efficiency improvement; and $26,270 lower cost to train new operators. | A transferable example of connecting equipment data with engineering and operational systems, but it is aerospace, not an automotive factory. These figures are case-specific and do not establish AI attribution or expected automotive results. |
| AMG Industries, NIST MEP case, 2024 | A US automotive supplier trialed a collaborative robot on a repetitive exhaust-tip manufacturing task. The case reports productivity rising 38%, from 200 manually produced parts per hour to an average of 276 parts per hour. The company later purchased a UR10E for that role. | An automotive example of task-focused automation and workforce redeployment, not evidence that AI caused the improvement. |
| Rimeco, NIST MEP case, 2025 | A collaborative robot was integrated with a Haas CNC mill, with real-time inspection algorithms calculating tooling offsets. The case reports $55,000 in new investment and $10,000 in cost savings. | A general-manufacturing example of automation and feedback, not an automotive AI result. |
The Magellan case also lists “payback at 0.5%,” but the available case description does not make the underlying calculation clear enough to interpret that figure as a general payback measure.
How to judge an architecture before expanding it
Compare implementation options against the same operational requirements rather than choosing on the basis of an AI feature list. A technically connected system can still fail to support a production decision if it does not carry usable context or fit the plant’s operating constraints.
Best Value
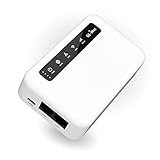
- 【SMART 4G TO WI-FI CONVERTER】Come with a standard nano-SIM card slot that can transfer 4G LTE signal to Wi-Fi networking. Up to 300Mbps (2.4GHz ONLY) Wi-Fi speeds. It can move into a 4G LTE wireless network if the Ethernet Internet fails, in order to ensure constant data transmission.
- 【OPEN SOURCE & PROGRAMMABLE】OpenWrt pre-installed, unlocked, extremely extendable in functions, perfect for DIY projects. 128MB RAM, 16MB NOR + 128MB NAND Flash. Dual Ethernet ports, USB 2.0 port, Antenna SMA mount holes reserved.
- 【SECURITY & PRIVACY】OpenVPN & WireGuard pre-installed, compatible with 30+ VPN service providers. With our brand-new Web UI, you can set up VPN servers and clients easily. IPv6, WPA3, and Cloudfare supported. Level up your online security.
- 【Easy Configuration with Web UI and GoodCloud】GoodCloud allows you manage and monitor devices anytime, anywhere. You can view the real-time statistics, set up a VPN server and client, manage the client connection list, and remote SSH to your IoT devices. The built-in 4G modem supports AT command, manual/automatic dial number, SMS checking, and signal strength checking in Web UI for better management and configuration.
- 【PACKAGE CONTENTS】GL-XE300-AF 4G LTE Portable IoT Gateway (2-year Warranty) X1, Ethernet cable X1, 5V/2A power adapter X1, User manual X1, Quectel EC25-AF 4G module pre-installed. Please refer to the online docs for first set up.
- Equipment compatibility: Can the solution connect to the actual installed machines and controls, including older equipment?
- Meaningful data: Can systems interpret identifiers, units, states, and events consistently, or will custom mapping remain necessary?
- Timing and reliability: Does collection and delivery meet the use case’s latency and availability needs?
- Cybersecurity and safety: Are data flows and access boundaries appropriate, and are any control actions governed by approved plant processes?
- Integration effort: What work is required to connect OT equipment with MOM and enterprise systems, and who will maintain those connections?
- Measured value: Does the result improve a baseline metric enough to justify implementation, support, and ongoing operating costs?
No single standard, gateway, twin approach, or AI service is established as the winner across automotive plants. The best fit depends on the equipment, data, systems, decision timing, risk boundaries, and economics of the specific use case.
What automotive AI evidence supports today
Hyundai Motor Company and Singtel announced an MOU on March 23, 2021, covering smart manufacturing and connectivity. The announcement described plans to develop and pilot a 5G-enabled smart-factory use case for HMGICS, with possible scaling across Hyundai plants, and separately described an IoT system for monitoring real-time EV-battery status and performance in Singapore. The announcement establishes intended work, not that the factory pilot was completed, scaled, or produced measured factory outcomes.
The available examples support an architecture-level case for better-connected manufacturing and illustrate selected integration and automation outcomes. They do not establish current, independently verified automotive-factory AI performance figures. Keep pilot announcements, research demonstrations, aerospace results, general-manufacturing cases, and measured automotive outcomes distinct when making investment decisions.
Free tools Windows power users keep installed
One-click scans. No signup required.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

